Wharve Diameter and Spindle Speed: What the Wharve Decides
Vindex technical notes · 02 Nov 2026
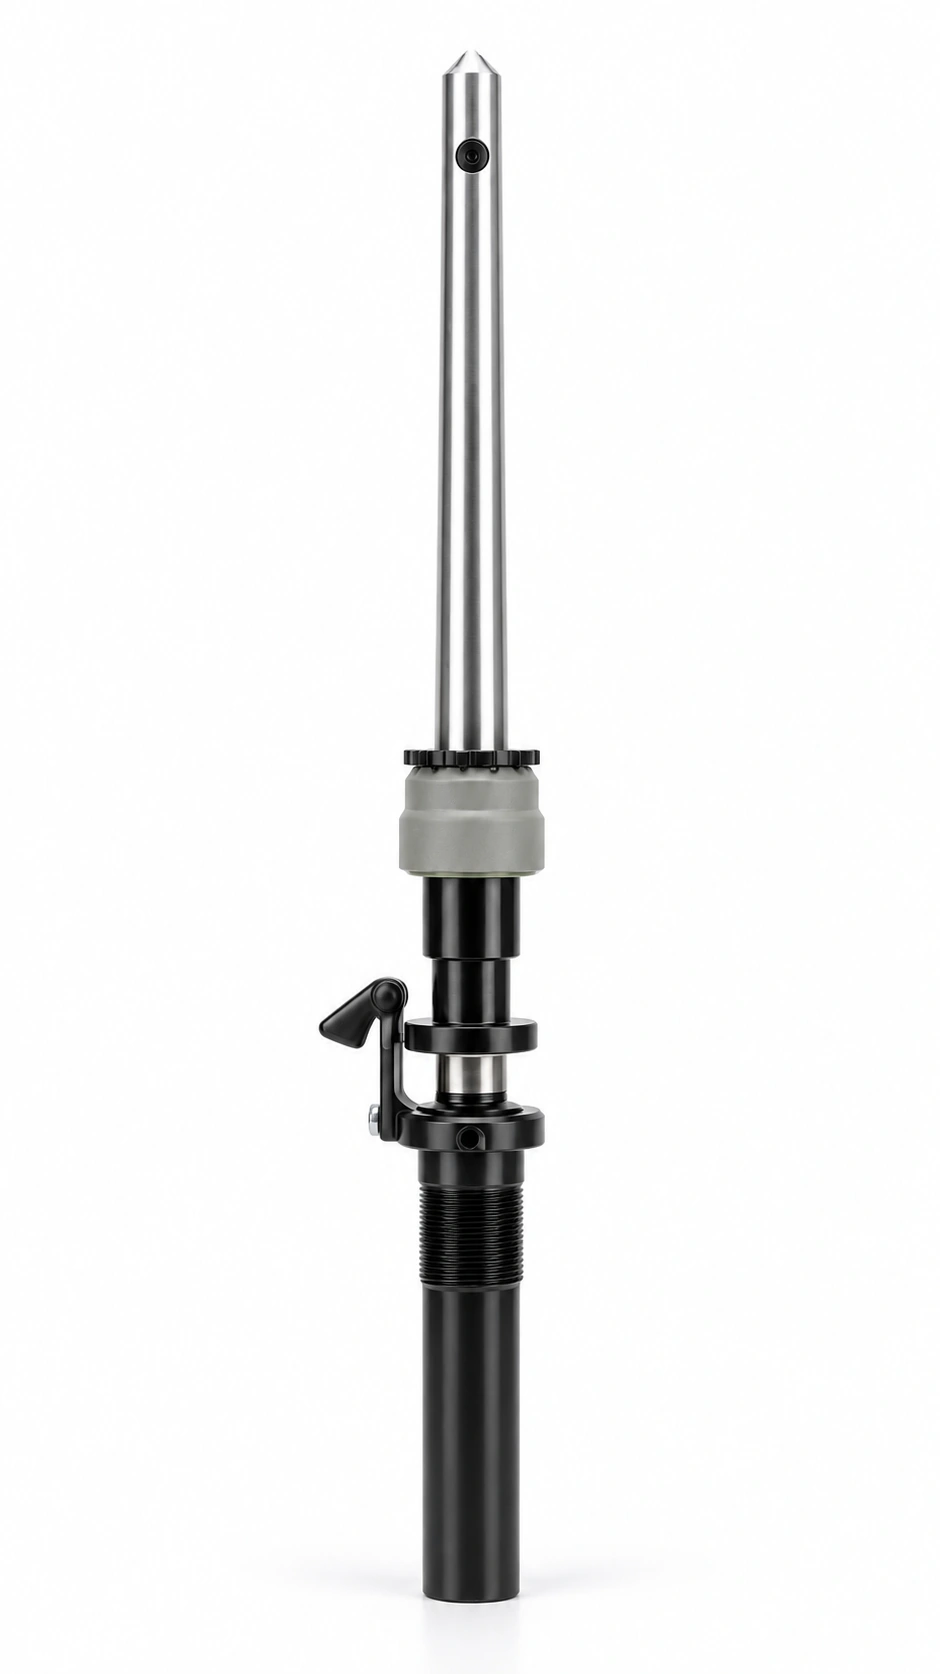
The wharve is the speed decision
Every ring-frame spindle carries a wharve at its base — the small grooved pulley that the driving tape runs on. The tape moves at the speed the frame sets, and the wharve turns that tape movement into spindle rotation. That makes the wharve diameter one of the things that decides how fast a spindle runs on a given frame.
A smaller wharve turns faster on the same tape drive; a larger wharve turns slower. This is why two spindles that look alike can run at very different speeds once fitted: the wharve diameter is doing the deciding. When a mill changes yarn count, ring diameter or frame speed, the wharve is one of the first dimensions checked, because it sits directly between the drive and the spindle.
Sourced wharve diameters
Vindex ring-frame spindle bolsters are listed with the following wharve diameters, taken from the product data:
| Bolster range | Wharve diameter |
| --- | --- |
| LMW ring-frame bolsters (HF-1, HF-21, HF-100) | 18.5–22 mm |
| HZ range bolsters | 25.4 mm and above |
The LMW range suits cotton, man-made fibre, wool and blend processing on compatible ring-spinning machines, with ring diameters of 38 / 40 / 42 / 45 / 48 mm and speeds up to 30,000 RPM. The HZ range covers winder, cops-winding, TFO and heavy-duty duties, with models HZ-33, HZ-44, HZ-55, HZ-66, HZ-68 and HZ-77, plus HZ 35. Wharve material in the product data is EN-24 steel.
No wharve diameter should be taken from a catalogue line alone. The exact diameter, groove profile and fit must be confirmed against the drawing for the machine and the spindle model being replaced.
What a wrong wharve does
A wharve that does not match the frame and the spindle model causes trouble that looks like other faults. The spindle may run at the wrong speed for the yarn being spun, the tape may slip or wear early, and vibration can appear at the spindle that was not there before. Yarn quality suffers before the cause is found, because the wharve is rarely the first suspect.
Matching the wharve also means matching the rest of the spindle: lift, ring diameter, tube length and blade. A wharve changed on its own, without checking the other dimensions, can leave the spindle sitting wrong in the bolster or the ring in the wrong place for the yarn path. The drawing settles all of these together, so it is the reference that matters, not any single dimension.
What to send with your enquiry
Send these details with your enquiry:
- Machine manufacturer, model and frame type.
- Current spindle or bolster model and wharve diameter.
- Ring diameter, lift and tube length.
- Yarn process — cotton, man-made fibre, wool or blend — and the running speed.
Vindex manufactures textile spindles and bolsters at Surendranagar, Gujarat, and exports textile machinery spares to spinning mills in 87 countries. Send your machine details and current wharve diameter, and the match will be confirmed against the drawing before a quotation is given.
Frequently asked questions
What does the wharve diameter decide? The wharve diameter is one of the things that decides spindle speed on the tape drive. A smaller wharve turns faster and a larger wharve turns slower on the same drive.
Which wharve diameters are listed? LMW ring-frame bolsters are listed at 18.5–22 mm and HZ range bolsters at 25.4 mm and above. Confirm the exact diameter against the drawing before ordering.
Where Vindex supplies: 87 countries, all Indian states
Vindex Industries exports textile spindles and bolsters to 87 countries. Among the leading buyer markets are Bangladesh, Turkey, Indonesia, Vietnam, Uzbekistan, Pakistan and Egypt, alongside mills across Asia, Africa, the Middle East, Europe and the Americas. Country-level export pages: Export-country directory
---
Checking a wharve size or matching a spindle to your frame? Send your machine make and model and the current wharve diameter to Vindex Industries — WhatsApp +91 89805 05555, vindex@vindexindustries.com, or enquire at vindexindustries.com.
Frequently asked questions
Which bottom-roller conditions should maintenance cover?
Inspect flute condition, surface wear, eccentricity and contamination. The guide connects these checks with drafting consistency and periodic faults.
Why should fly and oil be removed from the drafting zone?
Contamination can interfere with consistent fibre control and roller contact. Include cleaning and inspection in the machine maintenance routine.
Choose the Correct Replacement Roller
After inspection, identify the machine process and the original roller drawing before ordering. Use the ring-frame bottom roller page for ring-spinning positions, the roving / speed frame bottom roller page for simplex machines, or the fluted roller reference page to describe the working profile. Keep each roller position and quantity separate in the enquiry.