Spinning Fluted Bottom Roller
Fluted working surface for spinning machinery. Compatible with LMW, Rieter, Zinser, KTTM, Marzoli, Textool and Texmaco machines.
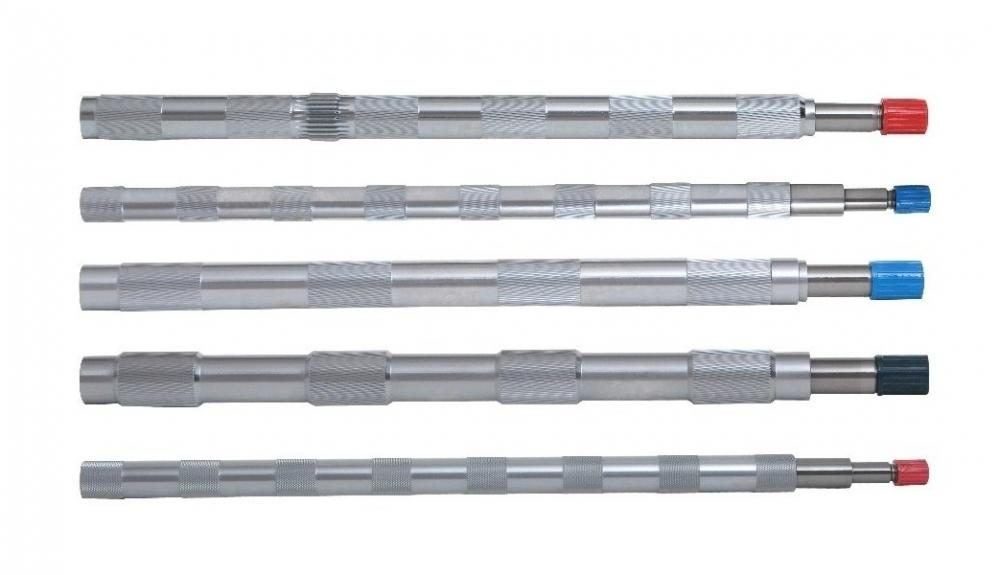
Application and construction
CNC-machined bottom roller for the named spinning-preparation or ring-frame application.
- Model
- DJ
- Material
- No.45 special carbon steel
- Roller diameter
- φ25 or φ27
- Dynamic pulsation
- ±0.02 mm; maximum ±0.03 mm
- Non-mechanical wave
- 98%
- Warranty
- 1 year
Features
- Fluted or herringbone / diamond knurled working surface as applicable
- Hard-chrome-plated finish
- Bending resistance increased by 9.1%
- Final section, flute, pitch and roller dimensions should match the machine drawing or sample.
Specifications
The fluted working surface is what grips the fibre in the drafting zone — flute depth, spacing and sharpness decide drafting control. This spinning fluted bottom roller is built with the flute geometry spinning machinery needs for positive fibre grip without fibre damage. Vindex Industries manufactures this bottom roller since 1985 at Surendranagar, Gujarat, exporting it to spinning mills in 87 countries in bulk order quantities.
It replaces the original fluted roller geometry directly. View the product specifications on this page for details.
When flutes wear smooth, drafting control slips away gradually — regular flute inspection catches the decline before it reaches the yarn.
Export markets
Vindex Industries manufactures this product in Surendranagar, Gujarat, and exports textile machinery spares to 87 countries — including Bangladesh, Vietnam, Turkey, Indonesia, Pakistan, Egypt, Uzbekistan, Brazil, Mexico and Thailand. Request an export quote.